If you’ve ever stood beside a running 5-axis machining center mid-job, watching it tilt, rotate, and carve a part from block to finished product with almost too-perfect precision, you might’ve wondered how it adapts so seamlessly to every material thrown at it. As the owner of a small, specialized 5-axis machining center supplier—one that’s spent 12 years tinkering, testing, and troubleshooting these machines for job shops and large aerospace firms alike—I get that question all the time. It’s not just about fancy code or moving parts, either; it’s about matching every component of the machine to the quirks of steel, aluminum, titanium, and the other tricky workpieces shops rely on. Let’s break down how these machines actually handle different materials, from the softest aluminum to the toughest heat-resistant alloys. 5 Axis Machining Center

First, let’s start with the basics: what makes a 5-axis machine different from a 3-axis? Where a 3-axis moves along X, Y, Z (left/right, front/back, up/down), a 5-axis adds two rotary axes—usually A (tilting around the X-axis) and C (rotating around the Z-axis). That freedom means you can machine a part from multiple angles in one setup, no re-clamping needed, which cuts down on human error and work-hardening—one of the biggest headaches when machining hard materials. But that flexibility only works if the machine’s parameters are tuned to the material at hand. Let’s start with the most common material in modern manufacturing: aluminum.
Aluminum is the workhorse of the automotive, aerospace, and consumer electronics industries. It’s light, durable, and machinable—on paper. But here’s the catch: pure aluminum is soft, and alloys like 6061 and 7075 have a tendency to “smear” during cutting. If the chip doesn’t break cleanly, it can weld itself back to the cutting tool, leaving a rough surface or even scratching the workpiece. So how does a 5-axis machine handle this? First, the spindle speed is key. For aluminum, we typically set spindle speeds anywhere from 1,500 to 15,000 RPM, depending on the alloy and the tool size. Too slow, and the tool rubs instead of cuts, causing that smearing effect; too fast, and the aluminum overheats, softening the surface unevenly. The rotary axes on a 5-axis machine help here too. Because you don’t have to re-clamp the part, you can use climb milling (where the tool spins in the same direction as the workpiece feed) almost exclusively, rather than conventional milling. Climb milling generates thinner chips that break off easier, reducing the chance of smearing. I’ve seen first-hand how a poorly tuned 5-axis machine will leave 7075 aluminum with a fuzzy, uneven surface, but when we adjust the rotary feed rates and tool path to match aluminum’s chip control needs, that same machine will produce smooth, tight-tolerance parts for drone frames or phone housings. Another thing we prioritize for aluminum: rigid tool holders. Since aluminum chatter (that high-pitched vibration that ruins surface finish) is common, we use heat-shrink holders or hydraulic holders instead of collets, which hold the tool more securely at higher speeds.
Next up: steel, specifically tool steel and stainless steel. This is where 5-axis machining really proves its worth over 3-axis. Steel is much harder than aluminum, has higher tensile strength, and generates a lot more heat during cutting. If you don’t manage that heat, the tool will wear out in minutes, or the workpiece will distort from thermal expansion. Let’s take 304 stainless steel, a staple in medical equipment and food processing parts. Machining stainless is tricky because it work-hardens so easily—if the tool edge gets too hot, the top layer of steel becomes harder than the rest of the part, so any subsequent cut will bounce off or cause a chip that’s not properly formed. The rotary axes on a 5-axis machine help here by allowing for continuous, consistent chip loads. Unlike a 3-axis machine, which might have to make awkward, angle-limited cuts that force the tool to take variable chip loads, a 5-axis can tilt and rotate the part to keep the tool engaged at a constant feed rate and depth. That consistency reduces heat buildup in the tool and workpiece. For tool steel (like A2 or D2, used in dies and molds), we crank up the rigidity of the machine and slow down the feed rates. Spindle speeds drop to 500–3,000 RPM, and we use carbide tools with specialized coatings (like TiCN or AlTiN) that can handle the friction. The big win here with 5-axis is that we can machine complex mold cavities in one setup, so there’s no error from re-clamping. I had a customer a few years back who was using a 3-axis machine to make injection molds for plastic toys; it took 12 setups, and every re-clamp added 0.002 inches of error. Switching to one of our 5-axis machines cut the setup time to one, and the part tolerance improved by 70%—that’s the kind of difference material-specific tuning makes.
Then there’s the big one: titanium. If aluminum is easy, steel is tough, titanium is the unforgiving heavyweight, used in aerospace turbine blades and medical implants. Titanium has a low thermal conductivity, meaning almost all the heat generated during cutting stays in the tool edge, not the chip. That heat will dull a tool in 10 minutes if you don’t plan for it, and titanium also work-hardens even faster than stainless. So how does a 5-axis machine handle this? First, the machine itself needs to be rigid—no flexing, no slop in the rotary axes. Titanium requires high cutting forces, so if the machine’s frame or spindle isn’t solid, it will vibrate, leading to broken tools and bad parts. We design our 5-axis machines with cast iron bases and direct-drive rotary axes to eliminate that slop, because even a tiny amount of play can send a shock through the tool when cutting titanium. Next, tool path strategy. For titanium, we use what’s called “helical ramping” instead of linear plunging. Linear plunging shoves the tool straight into the titanium, generating massive heat and force, but helical ramping lets the tool enter the material gradually, spreading the load. The rotary axes come into play here too; we can program the A and C axes to tilt the workpiece so the tool is always cutting at the optimal angle, reducing the contact area between tool and material and keeping chip loads consistent. Spindle speeds for titanium are even lower than tool steel, usually between 100–1,500 RPM, and we use solid carbide tools with specialized coatings (like diamond-like carbon, DLC, or AlTiN with extra thickness) and flood coolant directed right at the cutting edge. I’ve had aerospace customers tell us that their old 3-axis machines could only machine one turbine blade insert per tool, but with our 5-axis machines, they get three or four inserts per tool—saving thousands in tool costs and downtime.
Wait, what about materials that aren’t metals, too? A lot of modern manufacturing uses composites, like carbon fiber reinforced polymer (CFRP), used in airplanes and race cars. CFRP is abrasive, so it dulls tools super fast, and it can delaminate if the cutting force is too high. 5-axis machines handle this by using very high spindle speeds (up to 20,000 RPM) with small-diameter tools, and slow feed rates to minimize force. The rotary axes help here because we can machine along the fiber direction, reducing the chance of delamination, instead of cutting across the fibers which is harder on both the tool and the part.
But here’s the thing: it’s not just the machine’s hardware that makes this work. It’s the software too. Most of the job shops I work with come to us with 3-axis programming experience, and they have to learn how to program the 5-axis rotary axes to match the material. If you program a 5-axis machine to take a deep cut in aluminum with the same parameters you’d use for titanium, you’re going to get a broken tool or a scrap part. That’s why we don’t just sell machines—we provide training and customized parameter libraries for each material, so our customers don’t have to figure that out on their own.
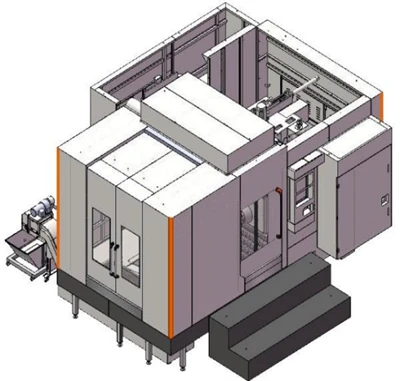
I think a lot of people look at 5-axis machining as a “better 3-axis” machine, something that just does the same job faster. But after 12 years in this business, I know it’s more than that. It’s a system that has to adapt to the material in front of it, whether that’s a soft aluminum drone frame, a hard stainless mold, a tough titanium turbine blade, or a brittle CFRP panel. Each material has its own quirks, and a good 5-axis machine—paired with the right programming, tooling, and expertise—can work with those quirks, not against them. If you’re a job shop looking to upgrade your machining capacity, or a manufacturer tired of scrap parts and slow production, we can walk you through exactly how our 5-axis machines can handle your specific materials, from prototype to full production runs. Reach out to us to start a conversation about your machining needs—no pressure, just real advice from people who’ve been in the shop floor with these machines every day for over a decade.
Gantry Machining Center References:
- Webster, J., & Day, M. (2016). Metal Cutting: Principles and Practice (2nd ed.). Industrial Press.
- Krzyżak, A., et al. (2020). Machining of Advanced Materials: From Alloys to Composites. Springer.
- Altintas, Y. (2012). Manufacturing Automation: Metal Cutting Mechanics, Machine Tool Vibrations, and CNC Design (2nd ed.). Cambridge University Press.
- Tóth, T., et al. (2018). 5-Axis Machining: Technology, Programming, and Applications. Hanser Publications.
Taizhou Qiyang Trading Co., Ltd.
As one of the most professional 5 axis machining center manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy bulk 5 axis machining center for sale here and get quotation from our factory. Customized orders are welcome.
Address: Zhenhai Village, Binhai Town, Wenling City, Taizhou City, Zhejiang Province
E-mail: qycncmachine@outlook.com
WebSite: https://www.qycncmachine.com/
