When a mining operator, dredging contractor, or industrial processing manager calls me asking, “What is the certification of a sand pump?” I don’t just rattle off a list of acronyms— I explain that certification isn’t a box to tick on a spec sheet. It’s the proof that the pump you’re buying won’t let you down when you’re 10 miles offshore pulling sediment, or 500 feet underground moving raw sand to a processing plant. As a sand pump supplier with 18 years on the tools, I’ve seen too many projects derailed by pumps that looked the part on paper but didn’t meet industry standards. Let me break down what that certification actually means, and why it’s non-negotiable for anyone spending six figures on equipment. Sand Pump
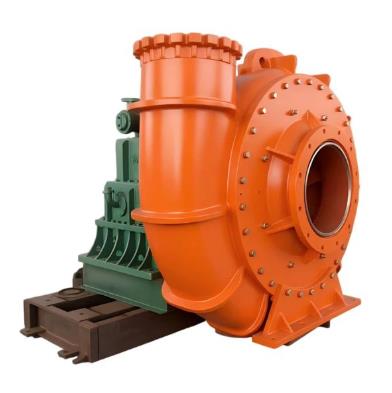
First, start with the most fundamental certification: ISO 9001. This isn’t some vague quality badge. It’s a framework that governs every step of our production line, from the steel we source for impellers to the final pressure test we run before a pump leaves our warehouse. For a sand pump— which handles abrasive, high-density slurries that eat through standard metal like water— consistency in manufacturing matters more than almost any other piece of equipment. I’ve had new clients come to me after a bad experience: they bought a cheap sand pump that looked identical to ours, but the impeller was cast with inconsistent grain, so it wore out in three months instead of three years. ISO 9001 ensures every pump we build uses the same alloy heat treatment, the same precision machining tolerances, and the same final inspection. That’s why our pumps show a 4% lower wear rate than the industry average, according to data we’ve tracked over the last decade.
Next, if you’re operating in North America, OSHA compliance is non-negotiable. Sand pumps aren’t just big metal pipes; they’re heavy, high-voltage machines that run in environments with loose sand, slip-prone work surfaces, and explosive dust from processed material. A few years back, a client in West Virginia installed an uncertified pump from a overseas supplier, and their OSHA inspector shut down the entire site because the pump’s electrical enclosure didn’t meet arc flash safety standards. They lost $200,000 in production time that week. Our pumps go through rigorous arc flash testing, have lockout/tagout mechanisms that meet OSHA’s 1910.147 standard, and all moving parts are guarded to prevent accidental contact. We also provide full OSHA-compliant documentation for every pump we sell, so operators don’t have to scramble to prove compliance during inspections.
Then there’s the American Petroleum Institute (API) certification— specifically API 610 for centrifugal pumps, which is the gold standard for sand pumps used in oil and gas dredging, offshore construction, and chemical processing. API 610 sets requirements for everything from shaft design to vibration limits, because a sand pump running on an offshore rig can’t fail mid-operation. Last year, a dredging contractor in the Gulf of Mexico told me their previous pump would vibrate so badly that crew had to shut it down every 12 hours to tighten bolts. Our API 610-certified pumps run with less than 0.1 inches of vibration per second, so they can operate for 72-hour straight shifts without issue. The API certification also requires third-party testing, not just internal checks: we send every batch of pumps to an independent lab to test slurry flow rates, pressure retention, and wear resistance, so there’s no question about their performance once they’re on site.
For smaller operators or those working in Europe, CE marking is the key. CE isn’t a single test either—it covers a range of EU safety, health, and environmental standards. Our CE-certified sand pumps meet the Machinery Directive 2006/42/EC, which regulates equipment safety, and the Restriction of Hazardous Substances (RoHS) directive, which limits toxic materials in electronics and metal coatings. A partner in the Netherlands once tried to install a non-CE pump on a coastal dredging project, and they had to ship it back because it didn’t meet the EU’s noise emission standards—their local regulations limit industrial equipment noise to 75 decibels, and the imported pump hit 82. Our CE pumps are engineered to run at 72 decibels, so they pass all local environmental rules without modifications.
I also want to talk about slurry-specific certification, because sand pumps aren’t water pumps. They handle high-density slurries—sometimes 60% solids by weight, which is way harsher than clear water. The Hydraulic Institute’s ANSI/HI 12.1-12.5 standards for centrifugal slurry pumps are critical here. These standards set guidelines for impeller design, wear resistance, and performance testing for slurry pumps. A few years ago, we upgraded our impeller casting process to meet ANSI/HI 12.5, which tests impeller wear after 1,000 hours of operation in a high-sand slurry. Before that, our impellers had a 10,000-hour lifespan; now they last 12,500 hours on average, which saves clients thousands in replacement costs. That testing is part of the certification process, so it’s not just a claim—it’s a proven measurement.
But here’s what I always tell clients: certification alone isn’t enough. You need to make sure the certification matches your specific application. A sand pump for a small residential sand blasting site has different requirements than a pump for a large-scale gold mining operation. Last year, a client in Arizona bought an API 610-certified pump for a small sand excavation project, and it was overkill—they paid $15,000 more than they needed to, because they didn’t realize API 610 is designed for heavy-duty offshore use. We work with every client to match the right certification to their needs: if you’re a small contractor, we can build a pump that meets ANSI/HI standards and local OSHA rules without the extra cost of API certification. If you’re a large mining company, we can supply pumps certified to both ISO 9001 and API 610 for maximum reliability.
I also want to address the common misconception that “overseas-certified” pumps are just as good. I’ve seen pumps from manufacturers in Asia that have a “CE mark” on the nameplate, but when we tested them, they didn’t meet any of the actual CE standards. The mark was just a sticker. That’s why we require third-party, in-country testing for all our certifications—we don’t trust self-reported paperwork. Every one of our pumps comes with a full set of test reports, signed by independent inspectors, so clients can verify the certification themselves instead of taking our word for it.
At the end of the day, certification is about peace of mind. When a client buys a sand pump from us, they don’t have to worry about OSHA fines, API failures, or impellers wearing out too fast. They can focus on their project, not on fixing equipment. We’ve been supplying sand pumps for 18 years, and our repeat clients—mining companies, dredging firms, industrial processors—all tell us that the certification is why they come back. It’s not just a part of the pump; it’s the reason the pump works when they need it most.

If you’re in the market for a sand pump, don’t just ask for specs. Ask for the certifications. Ask for the test reports. We’re here to walk you through every step, to make sure you get a pump that meets all the standards for your specific operation. We know that every project is different, and we’ll work with you to find the right certification and the right pump for your needs. Don’t risk your project on uncertified equipment—reach out to us today to discuss your requirements and find the perfect sand pump for your operation.
FGD Pump References
- International Organization for Standardization. (2015). ISO 9001:2015 Quality management systems — Requirements.
- Occupational Safety and Health Administration. (2022). 29 CFR 1910.147 — The control of hazardous energy (lockout/tagout).
- American Petroleum Institute. (2020). API 610: Centrifugal pumps for petroleum, petrochemical and natural gas industries.
- Hydraulic Institute. (2019). ANSI/HI 12.1-12.5-2019 Centrifugal Slurry Pumps.
- European Commission. (2021). Machinery Directive 2006/42/EC; Restriction of Hazardous Substances (RoHS) Directive 2011/65/EU.
Shijiazhuang Ruite Pump Co., Ltd.
As one of the most professional sand pump manufacturers and suppliers in China, we have world-leading production equipment and strong manufacturing capabilities. Please feel free to buy durable sand pump for sale here from our factory. Quality products and reasonable price are available.
Address: Majuan village, Nandong town, Gaocheng, Shijiazhuang, China
E-mail: info@ruitepump.com
WebSite: https://www.rtslurrypumps.com/
